Industrial digitalization is powered by key technologies that are reshaping the sector:
- Artificial Intelligence & IoT → real-time data collection and analysis to optimize supply chains, reduce downtime machines, and enable predictive maintenance.
- Automation & Digital Twins → simulation of production processes in virtual environments to reduce costs, improve quality control, and accelerate time-to-market.
- Big Data & Analytics → data-driven decision-making to predict demand, manage resources more effectively, and increase production capacity by up to +18%.

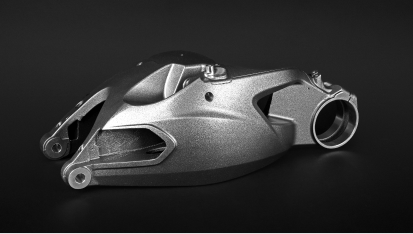
In this context, the VRM Group stands out as a case study in the integration of Industry 4.0 technologies applied to high-end manufacturing.
The company has developed a production model that combines technological innovation with environmental responsibility:
- Advanced Digitalization → interconnected systems to monitor every production phase in real time.
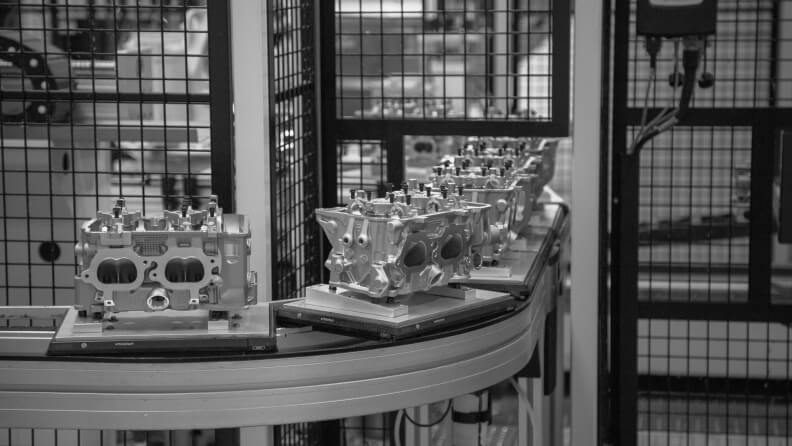
- Automation and Quality Control → high-efficiency production lines, integrated testing, and dedicated laboratories.
- Certified Sustainability → DNV GL standards for quality, environment, and safety, and ISO 14001 certification for environmental management.
Thanks to these investments, the VRM Group strengthens its position in luxury and automotive manufacturing Made in Italy, reinforcing an industrial approach based on technology, precision, and sustainability. The VRM Group will continue to play an active role in this transformation, confirming its position within a manufacturing system that looks to the future with efficiency, intelligence, and innovation.
This page is also available in: